
Commercial Brewhouse at a Glance
A commercial brewhouse is the hot-side production system that turns milled malt, water, and hops into cooled wort ready for fermentation. The best configuration depends on batch size, brews per day, vessel count, heating method, automation, cellar capacity, utilities, building access, and the brewery’s real weekly sales plan.
| Selection Factor | What to Confirm |
|---|---|
| Batch size | Actual hot-side working volume, target knockout volume, expected losses, and whether half or double batches are required. |
| Vessel configuration | Two-, three-, or four-vessel process and which brewing steps can overlap. |
| Heating | Electric, direct fire, or steam based on utility capacity, local cost, ventilation, heat-up time, and expansion plans. |
| Throughput | Real brews per day after mash, lauter, boil, whirlpool, transfer, cleaning, and operator constraints are included. |
| Automation | Recipe control, valves, pumps, flow meters, temperature, level, alarms, data logging, manual mode, and remote support. |
| Cellar match | Fermenter working volume, tank occupancy, double batching, maturation time, and packaging schedule. |
| Utilities | Peak steam or electrical load, hot/cold water, compressed air, cooling water, glycol where used, drainage, and wastewater. |
| Installation | Delivery route, floor loading, ceiling height, rigging, exhaust/steam management, service clearances, and commissioning. |
DME currently offers commercial brewhouses from 5 to 20 BBL with standard 5, 7, 10, 15, and 20 BBL sizes and options for half or double batches, while Ss Brewtech currently markets professional brewhouses from 5 to 20 BBL with steam or direct-fire heating. These are supplier-specific examples, but they show why buyers should compare batch flexibility as well as nominal barrel size. See DME 5-20 BBL Brewhouses and Ss Brewtech Pro Brewing.
Section 1: The Central Role of Thermal Process Engineering in Commercial Cellar Layouts
Running a modern brewery well starts with mastering the hot side of production.
For a growing brewery, handling malt sacks by hand and stirring open vessels is a real risk and an expensive bottleneck.
A clear understanding of the engineering behind a modern commercial brewhouse is the foundation for scaling any beer brand.
Every fermentation in the cellar depends on an efficient, predictable hot-side process to make good wort.
If sugars and proteins are not converted well during the first heating steps, your fermentation will fail.
These problems cause bad flavors, poor shelf life, and odd attenuation that can hurt a brand’s name.
A professional hot-side setup removes the manual errors of small-scale brewing.
Whether you run a local taproom or a large packaging floor, your hot-side machinery sets your margins.
This guide breaks down the fluid mechanics, layouts, and designs needed to build a strong hot-side system.

Section 2: Mechanical Fluid Flow and the Technical Elements of Extraction Loops
To keep your beer quality steady across thousands of barrels, you need a well-planned heating schedule.
The core process pulls starches from crushed grain and turns them into fermentable sugars using hot water.
High-pressure pumps push water through grist hydrators, wetting the crushed malt evenly before it enters the main tank.
Before the liquid moves to the fermentation cellar, the hot-side gear must run several temperature steps perfectly.
The liquid enters the vessels through automatic valves, where mixing blades gently turn the heavy grain mash.
These blades keep the whole volume moving at a steady speed without tearing the grain husks apart.
The spent grains are then separated in a filter vessel, where a false bottom holds the grain bed while the sweet liquid drains.
To study vessel design, filtration speeds, and sanitary fluid flow, engineers use the standards of the European Hygienic Engineering & Design Group (EHEDG).
Lauter Rakes and Spent-Grain Plows
The grain bed must stay open enough for wort to flow without being torn apart.
A commercial lauter tun can include a motorized rake-and-plow assembly.
The rakes move through the grain bed to break compacted spots, improve drainage, and give a more even extraction.
Their height and speed should be adjustable so the operator does not disturb the bed too much.
After lautering, the same assembly uses plow blades to push the spent grain toward the discharge door.
This cuts manual labor and shortens the time to prepare the vessel for the next batch.
Whirlpool Vessel Geometry
A poorly shaped whirlpool can leave the brewer with an unstable pile of trub and wasted wort.
Whirlpool performance depends on more than pump power.
A wide vessel with moderate height supports steady rotation and lets solids gather near the center.
A shallow dish bottom can make a tighter trub cone than a deep conical bottom.
The tangential inlet must bring the wort in smoothly, without too much turbulence.
Keep the clear-wort outlet away from the trub cone, so you can draw off clean wort without pulling hop and protein deposits into the heat exchanger.
Evaluate Whirlpool Performance by Wort Recovery and Trub Separation
Whirlpool design should be judged by more than whether a visible trub cone forms. The useful questions are how much clear wort can be recovered, how much trub reaches the cooler, how long settling takes, and whether the system performs across different hop loads and batch sizes.
GEA currently offers dedicated whirl-separation systems specifically designed around hot-trub removal and flexible brewery configuration, reinforcing that whirlpool geometry, inlet design, residence time, and outlet position should be treated as process-engineering decisions rather than cosmetic vessel details. See GEA WORTSTAR Whirl.
Section 3: Digital Automation Architecture and Parameter Regulation
Moving away from manual floor work means putting in a modern turnkey brewhouse control network.
The core system uses air-driven flow valves, steam jacket loops, digital flow meters, and variable-speed pump controllers.
The main PLC panel watches temperatures, pressures, and fluid densities in real time during the extraction loop.
If a temperature drifts anywhere in the heating loop, the software adjusts the steam valves at once to correct it.
Automated control removes human error from daily hot-side work, preventing boil-overs or ruined batches of wort.
By trusting the software to control your heating rates, you keep your recipes identical week after week.
This precise control makes sure every batch leaving the whirlpool matches your target gravity, protecting consistency.
To study malt starch conversion, enzymes, and raw ingredients, managers read journals from the American Society of Brewing Chemists (ASBC).
Automating Liquor Blending and Sparging
Good automation connects the brewing steps instead of controlling each vessel on its own.
Brewhouse automation can control more than vessel temperature and pump speed.
The system can blend hot and cold water to reach the right strike temperature before mash-in.
It can also manage wort recirculation, the wort grant, sparge-water flow, lauter-to-kettle transfer, whirlpool transfer, and knockout to the fermenter.
The brewer picks the recipe, and the system prepares the strike water, controls sparging, transfers the wort, and manages the final knockout.
Automating these steps cuts manual valve changes and keeps water additions the same from batch to batch.
Recipe Flexibility and Partial Batches
A system built only for full batches can limit experiments.
Judge a brewhouse across the full range of batch sizes you expect to make.
Pilot beers, seasonal products, and slow sellers may not need a full vessel.
The heating surfaces, temperature probes, agitators, pumps, and level controls must still work with a smaller volume.
The control system can store recipe settings for mash temperatures, rest times, transfer speeds, and boil schedules.
Checking minimum working levels and recipe storage before you buy lets one brewhouse handle both regular and specialty batches.
Define the Minimum and Maximum Validated Batch Size
Partial-batch flexibility should be tested against the physical vessel and control limits rather than assumed from the nominal brewhouse size.
| Partial-Batch Check | What Can Become Limiting |
|---|---|
| Mash vessel | Agitator coverage, temperature-probe immersion, grist-to-water ratio, heating surface, and minimum liquid level. |
| Lauter tun | Grain-bed depth, rake position, false-bottom coverage, runoff control, and sparge distribution. |
| Kettle | Minimum heating-surface coverage, boil vigor, evaporation control, foaming, and level measurement. |
| Whirlpool | Tangential-inlet performance, rotational velocity, trub collection, and clear-wort outlet position. |
| Automation | Level-sensor range, flow-meter accuracy, recipe limits, valve logic, and alarm thresholds. |
DME specifically lists half- and double-batch capability among the brewing options for its current 5-20 BBL commercial systems. Ask the supplier to state the validated minimum and maximum batch sizes for the exact configuration being quoted.
Section 4: Operational Economics and Scale Selection Metrics
Sizing your hot-side gear means looking at hard financial data and your expected weekly output.
For startup nano breweries or recipe labs, a compact 1 bbl brewing system gives a low-risk testing setup.
These small pilot systems let your team test new ingredients without wasting thousands of dollars in materials.
But if your plan relies on high-volume wholesale, a pilot setup will quickly cause bottlenecks.
A mid-size setup lets a growing brand scale its output without adding daily labor.
By cutting turnaround times, your facility can make several high-volume batches in one eight-hour shift.
This boost in equipment use lets ambitious regional companies scale packaging without doubling their floor space.
To review system balance math and water-use charts, engineers study the archives of the Brewers Association.
Matching the Brewhouse to Fermenter Capacity
A beautiful brewhouse sits idle when every fermenter is full.
A larger brewhouse does not raise output when the brewery has no free fermenters.
Plan the hot-side capacity together with your fermentation and maturation capacity.
As a rough guide, total fermenter volume may equal about six to ten times the brewhouse batch size.
The exact ratio depends on fermentation time, beer styles, expected sales, double-batching, and brewing days per week.
Keep enough separate tanks free to run the brewhouse while earlier batches keep fermenting.
Match Brewhouse Capacity to the Cellar Schedule, Not One Fixed Ratio
The six-to-ten-times fermenter-volume guideline above can be a rough planning reference, but it should not be used as a universal sizing rule.
A better production relationship is:
Weekly hot-side capacity = brewhouse batch volume × brews per day × brew days per week.
Then compare that output with fermenter working volume, average tank occupancy, recipe mix, maturation time, double-batch strategy, packaging days, and reserve capacity.
If a 10 BBL brewhouse usually double-batches into 20 BBL fermenters, for example, the cellar schedule should be modeled around two turns per fill and the time those 20 BBL tanks remain occupied. The hot side should not be expanded until fermentation, conditioning, cold storage, and packaging can absorb the extra wort.
Section 5: Purchasing Strategy and Procurement Safety Protocols
Sourcing your main processing gear means balancing startup capital against long-term maintenance costs.
Browsing verified brewhouse equipment for sale helps buyers find reliable machines at lower upfront prices.
Buying used gear from closed breweries can save thousands, freeing funds for packaging machinery.
But used parts need great care, since hidden cracks in steam jackets or pitted welds can cause serious failures.
New custom systems come with warranties, direct technical support, and modern wiring that meets local codes.
A good compromise is often buying new core vessels while sourcing used secondary storage tanks.
Whatever path you choose, checking the metal quality of every liquid-contact surface prevents costly contamination later.
Commissioning and Operator Training
Delivery is not the end of a brewhouse project.
The purchase contract should spell out what happens after the brewhouse reaches your building.
Commissioning usually includes checking utilities, testing pumps and valves, confirming sensor calibration, inspecting safety functions, and running water through every route.
Operators should get practical training on recipe controls, manual operation, alarms, cleaning, maintenance, and emergency steps.
A supervised first brew can reveal transfer, heating, or workflow problems that a factory test misses.
You should also receive updated drawings, manuals, spare-parts lists, and backup copies of the control software.
What a Brewhouse FAT and SAT Should Cover
| Stage | Typical Checks |
|---|---|
| Factory Acceptance Test | Vessel fabrication, piping, pumps, valves, agitators/rakes, instruments, control panel, recipe logic, alarms, safety functions, and utility connections. |
| Site Acceptance Test | Actual steam/electrical service, water, compressed air, drains, cooling water, ventilation, field piping, real heating rate, pump duty, and control integration. |
| Water commissioning | Fill, heat, transfer, recirculate, lauter-path simulation, boil control, whirlpool routing, knockout, drainage, and CIP without risking product. |
| First-brew commissioning | Mash-in, temperature stability, runoff, extraction, boil, evaporation, trub separation, cooling, oxygenation if included, yield, and operator workflow. |
| Handover | As-built drawings, manuals, spare-parts list, PLC/HMI backups, passwords/access rights, calibration records, training, and warranty contacts. |

Section 6: Comparing Multi-Vessel Vessel Topologies
The best layout for your hot side depends on your daily goals, space, and budget.
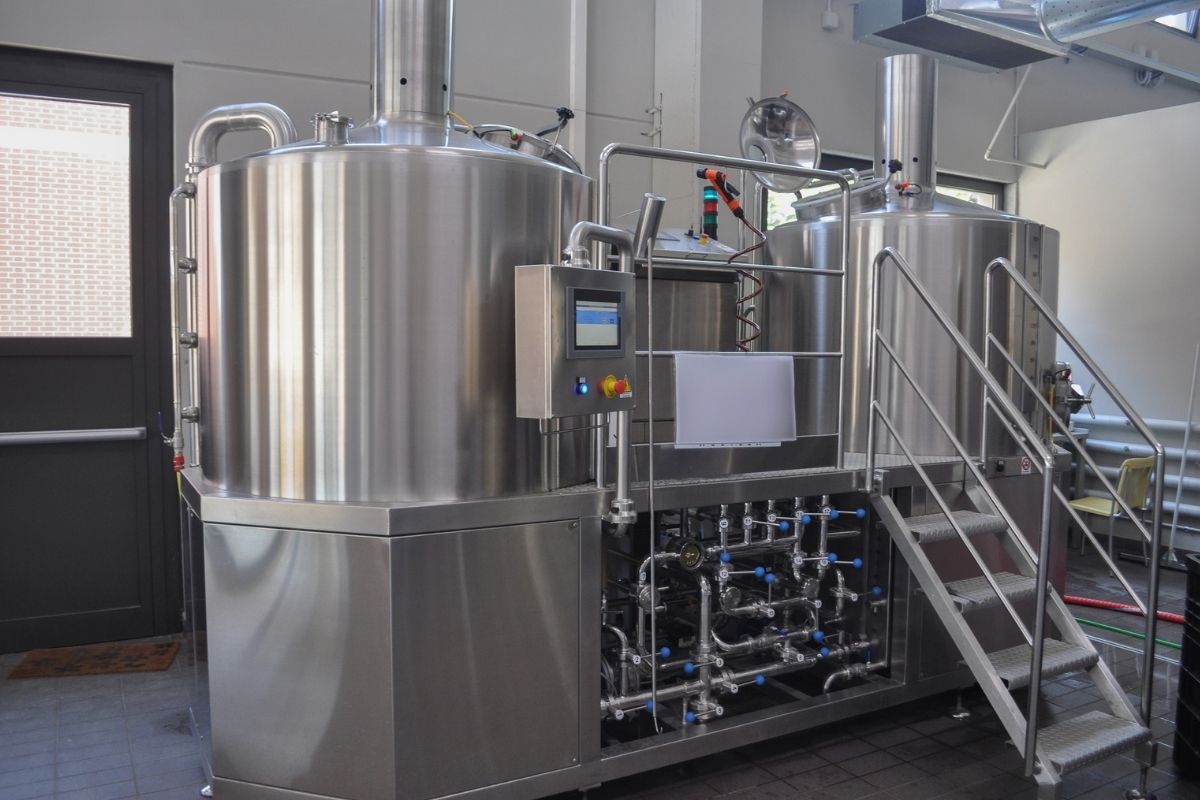
A classic 3 vessel brewing system splits the hot side into a mash mixer, a lauter tun, and a boiling kettle.
This setup lets your team start a second batch of wort while the first is still boiling.
By running these steps at the same time, your facility can finish three to four full batches in a day.
Smaller taprooms often combine functions into two-tank systems to save space, but that limits you to one batch at a time.
For multiple shifts, a multi-vessel design is the single best way to raise your yearly output.
Understanding these layouts helps directors pick the right system for their space.
The Four-Vessel Brewhouse Configuration
A separate whirlpool may look like a small upgrade, but it removes an important bottleneck.
A four-vessel brewhouse uses a dedicated mash mixer, lauter tun, brew kettle, and whirlpool vessel.
Separating every main hot-side step lets different stages run at the same time.
While one batch is boiling, another can start lautering or mashing.
The kettle frees up for the next batch as soon as boiling ends, while the first wort clarifies in the whirlpool.
This makes four-vessel systems very useful for breweries that need several brews per day, though they need more floor space, piping, automation, and capital.
Two vs Three vs Four Vessel Brewhouse
| Configuration | Typical Process Arrangement | Main Advantage | Main Tradeoff |
|---|---|---|---|
| 2 vessel | Combined mash/lauter plus kettle/whirlpool, or another paired arrangement | Lower footprint and capital cost | More process overlap limitations and longer turnaround between brews |
| 3 vessel | Mash/lauter plus kettle plus dedicated whirlpool, or mash plus lauter plus kettle/whirlpool | Removes one major bottleneck and improves double-batch scheduling | More piping, controls, floor space, and cost |
| 4 vessel | Separate mash mixer, lauter tun, kettle, and whirlpool | Maximum overlap of major hot-side steps for repeated brewing | Highest footprint, utility demand, automation complexity, and capital cost |
Actual brews per day depend on recipe, lautering time, boil time, cleaning, staffing, and automation. Ss Brewtech documents a 10 BBL three-vessel installation where the dedicated whirlpool helps the brewery double-batch efficiently by freeing the kettle sooner; that is a useful example, not a universal throughput guarantee. See 10 BBL 3-Vessel Brewhouse Example.
Section 7: Sizing the Equipment for Taprooms and Small Microbreweries
Finding the right capacity keeps you from outgrowing your gear too fast or drowning in debt.
For neighborhood taprooms focused on local pints, an efficient 3 bbl brewing system gives the perfect balance.
This size lets your staff keep twenty draft lines fresh and varied without a huge warehouse.
It fits inside standard retail units, avoiding expensive renovations or very high ceilings.
For slightly larger taprooms that also keg for local bars, moving up to a 5 bbl brewhouse adds flexibility.
This capacity lets your crew fill a standard ten-barrel fermenter with just two back-to-back runs.
By choosing the right scale early, you keep startup costs low while leaving room to grow into wholesale.
Choose Brewhouse Size From Weekly Beer Demand
The number of taps alone should not determine brewhouse size. A three-barrel system can work very differently for a taproom brewing many rotating beers than for a brewery selling a few high-volume flagships.
A simple first-pass sizing relationship is:
Required brews per week = target weekly packaged + draft volume ÷ expected finished-beer yield per brew.
Then add realistic hot-side losses, cellar losses, seasonal peaks, cleaning time, staff availability, and reserve capacity before selecting the nominal brewhouse size.
Section 8: Mid-Scale Production Logistics and Distribution Targets
As local brands grow into regional names, their hot-side capacity must grow to feed supermarkets and liquor stores.
Moving up to a 7 bbl brewhouse lets your cellar team fill a twenty-one-barrel tank in one working day.
This setup is popular with regional taprooms feeding a growing off-site wholesale draft network.
If you need faster growth, a 10 bbl brewhouse gives you the power to run high-speed canning lines.
At ten barrels, your team can make over three hundred gallons of finished beer in every hot-side shift.
This jump in daily output cuts your energy and labor costs per gallon, raising your profit margins.
Do Not Size the Brewhouse From the Packaging Line Alone
A 10 BBL brewhouse can feed a canning operation, but canning-line speed does not determine hot-side size by itself.
The full production model should include fermenter turnover, conditioning time, brite-tank or unitank strategy, cold storage, packaging days, keg demand, raw-material handling, and finished-goods storage. A faster brewhouse creates no value when the cellar or packaging schedule remains the bottleneck.
To set safe wash temperatures and protect your staff, the Master Brewers Association of the Americas (MBAA) offers full cellar safety guides.

Section 9: Energy Thermodynamics and Utilities Infrastructure
Your main heat source for boiling and mashing sets your utility bills for the life of the facility.
A modern electric brewhouse heats your liquid with high-power immersion elements placed right inside the tank.
Electric systems are very efficient, because almost all of the heat goes straight into the liquid.
They also skip complex chimneys, expensive gas lines, and fire-suppression hoods inside the building.
This makes electric a favorite in urban areas where codes limit gas emissions and venting.
For large operations with heavy power limits, steam heating stays the standard for fast boils and precise control.
Balancing your local utility rates against your install costs keeps your production costs as low as possible.
Electric vs Direct Fire vs Steam: Compare the Whole Utility System
| Heating Method | Best Fit | Main Design Questions |
|---|---|---|
| Electric | Smaller systems, sites with strong electrical service, or buildings where combustion venting is difficult | Available kW, service upgrade cost, demand charges, element loading, controls, and future expansion. |
| Direct fire | Craft systems where gas service and compliant exhaust are practical | Burner modulation, stack/venting, combustion air, local code, heat distribution, and kettle-bottom maintenance. |
| Steam | Higher-throughput plants or sites already supporting a boiler and steam distribution | Boiler capacity, steam pressure, condensate return, water treatment, traps, piping, permits, and boiler-room cost. |
No heating method is automatically cheapest everywhere. DME currently offers electric, direct-fire, or steam kettle heating depending on site conditions and local utility costs, which is the right way to frame the decision. See DME Brewhouse Heating Options.
Recovering Heat Exchanger Water
Wort cooling makes a useful supply of warm water.
The cold water used by the plate heat exchanger absorbs heat while it cools the wort.
Instead of sending this warm water to the drain, return it to the hot liquor tank.
The recovered water already holds part of the energy needed for the next mash, sparge, or cleaning cycle.
This cuts heating time, water waste, and utility use.
The hot liquor tank should be big enough to hold the recovered water without interrupting the current brew.
Track Wort-Cooling Water as a Brewhouse Energy KPI
Recovering hot water from wort cooling works best when the next process can actually use the recovered volume and temperature.
Record cold-water inlet temperature, hot-water outlet temperature, recovered volume, knockout time, and HLT storage capacity. This shows whether the heat exchanger is transferring energy efficiently and whether the brewery is recovering more hot water than it can use.
Alfa Laval reported in a 2025 brewery case that a wort-cooler upgrade reduced cooling time by 25% and improved water and energy performance. Treat this as a site-specific supplier case rather than a universal saving. See Alfa Laval Craft Brewing Efficiency Case.
Kettle Steam Condensers and Venting Limits
A brewery in a basement or rented unit may not be allowed to cut a large vent through the building.
A steam condenser helps when you cannot install a normal kettle stack through the roof or wall.
This is common in basements, leased buildings, and urban spots with venting or odor rules.
The condenser uses cold water to turn kettle vapor back into liquid.
Size it for the real steam load and give it enough draw to keep condensate from falling back into the kettle.
The kettle also needs enough headspace to lower the risk of boil-over while the condenser runs.
Steam Condenser Water Demand Belongs in the Utility Model
A kettle condenser can solve a vent-routing problem, but it shifts part of the design burden to cooling water, drainage, heat rejection, and condensate management.
Before selecting one, ask for the required cooling-water flow and temperature, expected condensate volume, allowable backpressure at the kettle, cleaning procedure, and effect on total building heat and humidity. In some facilities, recovering useful heat from the condenser circuit may also be worth evaluating.
Section 10: Advanced Regional Scale Processing Systems
When a brand expands into grocery chains across many states, the facility must move to industrial systems.
A high-output 15 bbl brewhouse platform lets your crew fill thirty-barrel cellar tanks in a two-brew rotation.
This scale needs heavy-duty utilities, including dedicated steam boilers, large water lines, and big electrical services.
For regional operations chasing wide market reach, a full 20 bbl brewhouse gives serious manufacturing power.
At this level, manual grain handling is impossible, so you need grain silos, auger lines, and heavy spent-grain pumps.
If your long-term goal is continuous packaging across shifts, a 30 bbl brewhouse system is the ultimate solution.
This industrial scale lets a brand make tens of thousands of barrels a year, driving ingredient costs to the minimum.
Do Not Treat 30 BBL as the Automatic End Point
A 30 BBL brewhouse is one commercial scale, not an “ultimate” size for every brewery. The correct end point depends on annual demand, brews per day, fermenter sizes, packaging capacity, warehouse space, utilities, raw-material logistics, labor, and expansion strategy.
Industrial suppliers such as GEA design brewhouse systems around process units and required throughput rather than one universal barrel ceiling. GEA also identifies wort boiling as the most energy-intensive step in the brewhouse, which makes energy strategy increasingly important as hot-side capacity grows. See GEA Brewery Systems.
To study automated production models, cleaning loops, and fluid dynamics, teams check the archives of the Institute of Brewing & Distilling (IBD).

Section 11: Production Facility Infrastructure Matrix
Choosing your hot-side machinery means balancing upfront cost against daily throughput goals.
The reference below shows the footprints and production capacity of the different equipment tiers.
                     ┌──► Heating: direct electric elements
[1 BBL Pilot / Nano] ├──► Throughput: 31 gallons per batch
                     └──► Best for: recipe testing and research labs
                       ┌──► Heating: electric or direct-fire gas
[3 BBL to 5 BBL Craft] ├──► Throughput: 93 to 155 gallons per batch
                       └──► Best for: neighborhood taprooms and brewpubs
                           ┌──► Heating: direct-fire gas or low-pressure steam
[7 BBL to 10 BBL Expanded] ├──► Throughput: 217 to 310 gallons per batch
                           └──► Best for: high-volume taprooms and local wholesale
                              ┌──► Heating: high-pressure industrial steam boiler
[15 BBL to 30 BBL Industrial] ├──► Throughput: 465 to 930 gallons per batch
                              └──► Best for: regional distribution and automated canning lines
Section 12: Metallurgical Integrity and Clean-In-Place Loop Mechanics
The reactions between your ingredients and the tank walls directly affect your beer’s shelf life.
Commercial hot-side vessels must be made from strong stainless steel, usually AISI 304 or acid-resistant AISI 316L.
These alloys have plenty of chromium and nickel, which form a passive oxide layer that protects the metal.
This layer guards your tanks against cleaning acids, high-chlorine water, and the strong acidity of boiling hops.
To stop bacteria, the inside steel must be polished very smooth, with a roughness of 0.8 micrometers or less.
Rough patches, welds, or scratches can hide residue and shield wild yeast from normal cleaning.
To keep your layout safe and correctly piped, designs must follow the frameworks managed by the Deutscher Brauer-Bund.
Section 13: Facility Safety and Environmental Wastewater Frameworks
Running an industrial hot-side system means balancing intense heat and chemicals with strict local laws.
The high-pH caustic washes and low-pH acid rinses used to clean your kettles cannot flow straight into the city sewer.
To meet water safety laws, modern plants must fit a dedicated wastewater neutralization system.
This setup collects your spent cleaning solutions in a treatment tank and uses probes to balance the pH before discharge.
Your crew must also wear full protective gear, including chemical-resistant suits, heavy gloves, and face shields.
By making safety and the environment a priority, you protect your staff and avoid legal delays or fines.
Brewhouse Wastewater Requirements Are Site-Specific
The statement above that caustic and acid cleaning solutions cannot go straight to the city sewer is a useful conservative planning assumption, but actual discharge requirements depend on the local sewer authority, pretreatment permit, pH, flow, organic loading, temperature, and local limits.
The brewhouse utility plan should therefore include spent-grain solids management, high-strength wort or trub losses, CIP discharge, floor drainage, equalization, neutralization, and any sampling points required by the local wastewater program.
Planning the Complete Utility Supply
The vessels are the most visible part of the brewhouse, but the utilities decide whether they can work.
Brewhouse design must include the utilities that keep every vessel and control system running.
The utility plan should cover steam, refrigeration, compressed air, electrical power, water treatment, drainage, and data connections.
Work out peak demand for times when several pumps, heating zones, and cooling processes run together.
An undersized boiler, compressor, chiller, or electrical service can slow every batch, even when the tanks have plenty of capacity.
Leave spare capacity and easy connection points for future tanks or packaging gear, so expansion is less disruptive.
Calculate Utilities From Peak Simultaneous Demand
Utility sizing should use the busiest realistic operating condition, not the average daily consumption.
| Utility | Peak-Demand Inputs |
|---|---|
| Steam / electric heat | Mash heating, kettle boil, HLT recovery, CIP heating, simultaneous brews, and start-up demand. |
| Water | Mash liquor, sparge, wort cooling, cleaning, hose stations, packaging, and peak refill rate. |
| Compressed air | Pneumatic valves, actuators, instruments, packaging equipment, and simultaneous valve movement. |
| Electrical | Heating elements, pumps, augers, mill, controls, air compressor, chiller, packaging, and future loads. |
| Cooling | Wort knockout, cold liquor, glycol loads, cellar demand, and the required knockout time. |
| Drainage | Simultaneous vessel dumps, cleaning discharge, wort or product losses, condenser water, and floor washdown. |
A utility schedule should show connected load, expected operating load, peak simultaneous load, and expansion reserve for each service.
What to Compare in a Commercial Brewhouse Quote
A professional quote should define the complete hot-side production system and installed scope rather than only barrel size and vessel count.
| Quote Item | What to Confirm |
|---|---|
| Capacity | Working volume, knockout target, gross vessel volume, minimum batch size, double-batch capability, and expected losses. |
| Vessel configuration | Two-, three-, or four-vessel layout; combined functions; dedicated whirlpool; HLT/CLT; and process-overlap assumptions. |
| Heating | Electric/direct-fire/steam duty, heat-up time, evaporation assumptions, boiler or power requirements, condensate, and ventilation. |
| Mash / lauter | Agitator, rake/plow, false bottom, grain-out, grant, runoff control, sparge system, and high-gravity capability. |
| Boil / whirlpool | Boil system, hop additions, evaporation control, tangential inlet, trub separation, clear-wort outlet, and condenser if used. |
| Pumps and piping | Pump curves, VFDs, valve tree/manifold, sanitary design, pipe sizes, flow meters, drainability, and sample points. |
| Automation | PLC/HMI, recipes, user permissions, manual mode, alarms, data logging, remote support, backups, and plant integration. |
| Utilities | Steam/electric load, water, compressed air, cooling water/glycol, drainage, wastewater, and peak simultaneous demand. |
| Installation | Footprint, operating height, shipping route, rigging, floor loading, exhaust, foundations, field piping, and service clearance. |
| Acceptance and support | FAT, SAT, commissioning, first-brew support, training, documentation, warranty, spare parts, and response times. |
Current Brewhouse Price Snapshot
Ss Brewtech currently lists starting prices of $85,140 for 5 BBL, $88,000 for 7 BBL, $92,400 for 10 BBL, $115,610 for 15 BBL, and $131,450 for 20 BBL professional brewhouses. These are August 2026 supplier starting-price snapshots, not installed-project budgets; freight, utilities, rigging, installation, commissioning, local code work, and options can materially change total cost. See Ss Brewtech Brewhouse Starting Prices.
Brewhouse FAQ
What is a brewhouse?
A brewhouse is the hot-side brewery system used to mash, separate sweet wort from grain, boil, separate trub, and send cooled wort toward fermentation.
What is the difference between a 2-vessel and 3-vessel brewhouse?
A two-vessel system combines more process functions, reducing footprint and cost. A three-vessel system separates another major stage so operations can overlap and repeated brewing can be faster.
When is a 4-vessel brewhouse useful?
It becomes attractive when the brewery needs several brews per day and benefits from separate mash, lauter, kettle, and whirlpool vessels operating in overlapping stages.
How do I choose brewhouse size?
Start with required weekly beer volume and finished-beer yield, then calculate brews per week and check fermenter capacity, brewing days, labor, utilities, cleaning time, and seasonal peaks.
Should fermenter capacity be six to ten times brewhouse size?
That can be a rough planning range, but the correct cellar size depends on actual tank occupancy, beer styles, maturation, double batching, packaging schedule, and reserve capacity.
Is electric, direct fire, or steam better?
No heating method is best everywhere. Compare utility availability, installation cost, heating rate, local energy prices, venting, boiler requirements, maintenance, and future scale.
Can a commercial brewhouse make partial batches?
Some can, but the supplier should confirm the validated minimum working volume for heating surfaces, sensors, agitators, lauter geometry, pumps, and automation.
How many brews per day can a brewhouse produce?
It depends on vessel configuration, mash and lauter time, boil, whirlpool, cleaning, recipe, automation, staffing, and how many process steps can overlap.
What utilities should be sized before buying a brewhouse?
Confirm peak steam or electrical heating, water, compressed air, cooling, drainage, wastewater, ventilation, and the simultaneous load from other brewery equipment.
What should be included in a brewhouse quote?
Compare capacity, vessel configuration, heating, mash/lauter equipment, boil/whirlpool design, pumps, automation, utilities, installation, FAT/SAT, commissioning, training, warranty, and spare parts.
Section 14: Final Summary and Operational Growth Blueprint
Choosing your core setup needs a clear view of your sales goals, your space, and your budget.
If you run a taproom where beer moves fast on-site, a compact electric setup is an affordable start.
But if you want to grow wholesale across many states, a fully automated industrial steam skid is a must.
Check your building’s floor weight limits, balance your chemical strengths, and enforce strict validation loops.
Pick the right setup for your volume, treat your packaging line as a key partner, and your team can keep delivering great beer.
Contact Us

We help breweries around the world choose the right brewing technologies for every size and style.
Email: info@brewingmachinery.com
Vicenza, Italy
All rights Reserved Brewing Machinery | P.IVA 04501790242 | Privacy Policy | Cookie Policy | Blog Disclaimer

Author | Operations & Sourcing Lead
Luca is an operations and sourcing specialist with extensive experience in project management and industrial manufacturing. This blog serves as a technical resource for brewery owners, offering clear guidance on equipment design, quality control, and supplier evaluation. In parallel, Luca advises international buyers on sourcing and importing brewing equipment—helping them manage risk, avoid costly mistakes, and achieve consistent production quality.
