
Read Time: ⏱️ 10 minutes | By: Luca
Brewery CIP Skid at a Glance
A brewery CIP skid is a fixed or modular clean-in-place station that stores, heats, pumps, doses, routes, recovers, and monitors cleaning solutions for tanks, piping, heat exchangers, fillers, and other brewery circuits. The skid should be designed from the actual cleaning objects and operating schedule rather than annual beer volume alone.
| Design Factor | What to Confirm |
|---|---|
| Cleaning objects | Which tanks, pipes, heat exchangers, fillers, brewhouse vessels, and packaging circuits the skid must serve. |
| Simultaneous circuits | Whether one, two, or more cleaning loops must run at the same time without stealing flow, heat, or chemical inventory from each other. |
| CIP tanks | Number of vessels, working volume, water/caustic/acid/recovery duty, insulation, heating, drainability, and future expansion. |
| Supply and return pumps | Required flow, total dynamic head, air handling, hygienic design, VFD control, and the hydraulically worst circuit. |
| Heating | Steam or electrical duty, heat exchanger size, heat-up time, return temperature, and heat-recovery options. |
| Valve routing | Matrix or valve-cluster logic, feedback, interlocks, product/CIP separation, maintenance mode, and safe manual override. |
| Instrumentation | Temperature, flow, pressure, conductivity, level, chemical dosing, valve feedback, and calibration requirements. |
| Validation | FAT/SAT, spray coverage, worst-case circuit, acceptance criteria, cycle records, and revalidation triggers. |
Alfa Laval currently describes its brewery CIP Station as a modular skid-mounted plug-in unit for automated cleaning of piping, tanks, filling machines, heat exchangers, and other brewery equipment, with time, temperature, pressure, and flow adjustable to the cleaning object. See Alfa Laval CIP Station.
Section 1: Strategic Infrastructure Milestones in Plant Expansion
Running a modern brewery well means planning your cleaning setup as you grow.
For a growing brewery, cleaning and filling steel tanks by hand quickly becomes a bottleneck.
As a brewery scales up its weekly volume, moving from mobile setups to a permanent brewery cip skid is a key engineering milestone.
Every recipe made in the brewhouse depends on your cold-side cleaning to keep its flavor until it reaches the glass.
Cellar managers must decide when to replace their mobile utility pumps with a multi-tank central system.
Looking at your growing tank counts, daily wastewater limits, and how many loops run at once helps set the right timeline.
Whether you supply a small taproom or run high-speed packaging lines, your cleaning choices set your daily labor cost.
This guide breaks down the fluid mechanics, layouts, and economics of a permanent cleaning skid.
The right cleaning solution helps remove beer residue, yeast, sugars, and other buildup from brewery equipment.
Different cleaning methods can be used depending on the system, but the goal is always to keep tanks, pipes, and filling lines hygienic.
Good cleaning also helps prevent products from cross contaminate between batches, protecting the flavor, safety, and quality of the beer.
Checking the Skid Footprint and Delivery Route
The skid must fit through the brewery before it can fit inside the brewery.
The footprint of a CIP skid is more than just its tank size.
Leave enough room to inspect pumps, remove valves, replace seals, calibrate instruments, and safely reach the electrical cabinet.
Measure the full delivery route too, including doors, corridors, loading areas, ramps, and overhead obstacles.
A compact skid may use vertical space or a narrow frame to fit an existing cellar.
But cutting the footprint should never make routine maintenance unsafe or too hard.
Adapting the Skid to the Brewery Building
A skid can have the right capacity and still be completely wrong for the room.
A permanent CIP skid must be designed around the building where it will run.
The ceiling height can affect tank diameter and overall vessel shape.
Engineers should also check delivery doors, maintenance clearances, drains, utility connections, pipe routes, and access to pumps and valves.
When space is tight, lower and wider tanks can give the needed capacity without going over the height limit.
Finish these checks before the skid design is approved, to avoid expensive changes when the equipment arrives.
Design the Skid From the Approved Utility and Layout Drawing
The final general-arrangement drawing should include more than the footprint. It should show operating and maintenance clearances, full tank height, lifting points, valve movement, pump-removal space, heat-exchanger access, electrical-panel clearance, chemical delivery area, drains, utility headers, and every process connection leaving the skid.
Before approval, confirm steam or electrical capacity, water supply, compressed air, electrical service, floor drainage, wastewater routing, ventilation, floor loading, and the distance to the most remote cleaning object. Long distribution runs can materially change pump head and heat loss.
Section 2: Fluid Dynamics and Oxygen Protection in Clean-In-Place Protocols
Keeping your beer quality high over long trips means controlling liquid speed during the cleaning loop.
Oxygen and biological soils are the main enemies of raw packaged beer, causing contamination that destroys aromas.
To protect your flavor, a strong industrial layout uses a sealed process called clean in place inside the pipes.
Before any liquid enters the tank, the machine locks onto the process lines and runs a multi-stage cleaning program.
The cycle clears out the room air and replaces it with clean, pressurized gas.
Gas Purging Is a Separate Process Decision
The pressurized-gas step described above is not a universal requirement for a brewery CIP skid. Gas purging may be part of product recovery, oxygen control, drying, or process isolation, but it should be engineered separately from the basic cleaning hydraulics.
Any gas step must follow the vessel and pipe pressure ratings, approved valve sequence, venting design, gas-monitoring requirements, and the brewery’s safety procedure.
The system then matches the fluid pressure at the spray ball to the speed needed to scrub the tank walls well.
With the pressure balanced, the liquid flows smoothly down the tank wall, so it does not splash or lose control.
To study how flavor oxidation works in steel tanks, managers read resources from the Brewers Association.
Section 3: Digital Management Frameworks and Electronic Parameter Regulation
Moving away from manual cleaning means fitting a modern automated CIP system on your cellar floor.
The core system uses high-pressure pumps, air-driven flow valves, steam heat exchangers, and digital sensors.
The main PLC panel watches temperature, pressure, and chemical strength in real time during the wash.
If pressure drops anywhere in the fluid path, the system stops the loop at once and sets off an alarm.
Automated software removes human error from daily cleaning, preventing accidents or ruined batches.
By letting the software control the flow rates, you can be sure your cleaning loops run as designed every day.
This precise control makes sure every tank and vessel leaves the floor fully clean and ready for fresh beer.
To study wild yeast biology and draft-line hygiene, managers read journals from the American Society of Brewing Chemists (ASBC).
Using a Valve Matrix for CIP Routing
The valve matrix acts like the traffic controller of the CIP system.
A central CIP skid can use a valve matrix to route cleaning solutions to different production circuits.
The matrix connects water supplies, CIP delivery lines, return lines, pumps, heat exchangers, and process equipment in one controlled area.
The PLC opens the route it needs while keeping unrelated tanks and lines isolated.
Manual control should stay available for commissioning, maintenance, direct pump operation, and individual valve testing.
Safety interlocks must stop incompatible routes from opening at the same time.
Valve Matrix Design Should Include Positive Route Verification
A valve matrix is useful only when the automation can prove that the intended route is open and incompatible product or CIP routes remain isolated.
| Valve-Matrix Function | What to Confirm |
|---|---|
| Route selection | Which CIP supply and return paths are permitted for every cleaning object. |
| Valve feedback | The PLC confirms actual valve position rather than assuming the command succeeded. |
| Interlocks | Incompatible chemical, product, recovery, and drain routes cannot be opened together. |
| Mixproof separation | Where simultaneous production and cleaning require hygienic separation between adjacent paths. |
| Manual / maintenance mode | Controlled access for commissioning and service without bypassing critical safety protections. |
| Failure response | What happens after loss of air, power, position feedback, communication, or an unexpected pressure condition. |
GEA’s current CIP-STAR concept uses mixproof valves to separate vessel groups and pipes so they can be cleaned independently even while production continues elsewhere. See GEA CIP-STAR Brewery System.
Section 4: Microbiological Quality and the Science of Process Loop Sanitation
To protect your beer’s flavor over long supply chains, you must keep full biological control.
The process of modern cip brewing works by combining strong mechanical force with strong chemical cleaners.
When hot wort or fruit juice runs across steel sheets, it leaves organic soils that shield microbes.
If these soils are not fully dissolved during your wash, bacteria like Lactobacillus quickly take hold.
These infections cause bad off-flavors, cloudy beer, and sudden bottle pressure spikes that can ruin your name.
An automated loop drives cleaners deep into hard-to-reach spots, like valve seats and pipe welds.
The fast fluid flow creates a strong scrubbing action on the pipe walls, lifting films and sweeping them to the drain.
To review wash-line schematics and design rules, engineers use the European Hygienic Engineering & Design Group (EHEDG).
Section 5: Analyzing Manual Scrub Protocols vs Automated Configurations
Deciding how to spend your weekly cleaning hours starts with hard financial data.
Running the numbers on a manual cleaning vs cip brewery setup helps directors plan for growth.
Hand spray-down methods need constant labor, waste huge amounts of water, and expose your crew to strong chemicals.
Hand scrubbing also cannot safely reach the high walls of large modern tanks.
A sealed automated loop uses far less chemical because it recirculates the solution over a set time.
By cutting tank turnaround from six hours to forty-five minutes, you can run more batches per week.
This big boost in tank use lets fast-growing brands scale up without buying more fermenters.
Do Not Use One Universal CIP Turnaround Time
The six-hour-to-forty-five-minute example above can illustrate the potential production benefit of automation, but it is not a universal result for every skid or brewery.
Actual turnaround depends on circuit volume, heat-up time, soil, spray device, chemical program, flow, rinse endpoints, recovery logic, validation, operator setup, and any COP work that remains.
The financial case should compare the same cleaning objects before and after the skid project using measured labor, utilities, wastewater, cycle time, tank availability, and verification results.
Heat Recovery in a Brewery CIP Skid
A hot solution still holds valuable energy when it returns from the cleaning circuit.
A regenerative heat exchanger can recover part of that heat from the hot returning liquid.
The recovered heat can preheat incoming water before the next cleaning phase starts.
The boiler or steam system then needs less energy to bring the new solution up to temperature.
Heat recovery is especially useful in breweries that run several CIP cycles every day.
The design must prevent cross-contamination between the returning solution and the incoming clean water.
Heat Recovery Must Be Designed as a Hygienic Utility Function
Heat recovery can reduce steam or electrical demand, but the exchanger and piping must preserve hygienic separation between dirty or chemical return streams and clean utility water.
The business case should compare recoverable temperature difference, daily cycle count, heat-exchanger effectiveness, fouling, cleaning requirements, pump energy, maintenance, and the cost of the recovered heat.
Do not add heat recovery only because the return is hot. A low cycle frequency or small temperature difference may not justify the extra equipment and controls.
Section 6: Dissecting the Elements of a Complete Brewery Packaging System
Running an efficient packaging floor means joining several sub-systems into one smooth workflow.
A professional brewery cip system is more than the filling valves and intake manifolds.
The setup uses a network of chemical dosing pumps, steam boilers, gas regulators, and heavy-duty conveyors.
The main PLC panel watches temperature and pressure live and changes flow rates to prevent foaming.
If a returned vessel shows an odd pressure drop, the software flags it and halts the line.
This constant checking keeps dirty or damaged vessels out of the filling loop and protects your whole batch.
To balance smart controls with classic quality, teams read technical archives from the Siebel Institute of Technology.
Preassembly and Factory Testing
Finding a control or piping problem at the factory is much easier than after the skid is installed.
A brewery CIP skid can be assembled and tested at the maker’s facility before delivery.
Factory testing confirms that pumps, valves, sensors, controls, alarms, and cleaning sequences all work.
Check the skid’s utility needs, connection points, dimensions, and control interfaces before shipment.
A preassembled plug-in design cuts installation work and shows technical problems before the gear reaches you.
A tested skid arrives with most mechanical and electrical work done, so you can connect utilities and commission with fewer delays.
Factory Acceptance Test and Site Acceptance Test Checklist
Factory testing and site commissioning should verify different parts of the project.
| Test Stage | Typical Checks |
|---|---|
| FAT – mechanical | Skid dimensions, tank fabrication, valves, pumps, heat exchanger, instruments, piping, weld finish, drainability, tags, and connection points. |
| FAT – controls | PLC/HMI, recipes, valve feedback, interlocks, alarms, manual mode, user permissions, data logging, and communication interfaces. |
| FAT – functional | Pump operation, simulated routes, dosing logic, heating sequence, level protection, emergency stops, and fault response. |
| SAT – utilities | Actual water, steam/electric heat, compressed air, electrical supply, drains, and wastewater interfaces. |
| SAT – hydraulics | Real flow, pressure, return behavior, heat loss, and worst-case remote circuits after field piping is connected. |
| SAT – validation | Approved cleaning recipes, spray-device duty, rinse endpoints, acceptance criteria, records, and operator training. |
Alfa Laval describes its CIP station as a modular skid-mounted plug-in design, but site testing is still important because field distribution piping and utilities determine the final operating conditions. See Alfa Laval CIP Station Product Leaflet.
The Skid Frame and Modular Installation
The skid frame is not just a platform under the tanks.
The main parts of the CIP system can be mounted on one structural frame.
This lets tanks, pumps, valves, instruments, heat exchangers, and control panels ship as one coordinated module.
Slide rails or a proper skid base make positioning and installation easier.
The frame must stay stable under the weight of full tanks and handle vibration from the pumps.
Leveling points matter too, because an uneven skid can hurt drainage, tank-level readings, and pump operation.
Check Skid Operating Weight and Center of Gravity
The structural review should use the skid’s operating weight with tanks full, not only shipping weight. The supplier should also identify lifting points, center of gravity, anchoring requirements, vibration loads, and any leveling tolerance needed for accurate tank-level measurement and complete drainage.
Designing the Distribution Piping Around the Skid
The skid is only one part of the cleaning system.
A powerful skid cannot make up for a poorly designed distribution network.
Long pipe runs, undersized lines, dead legs, wrong slopes, and trapped high points cut flow and leave solution in the system.
Size the supply and return piping for the required flow rate and the total pressure loss of the circuit.
The lines should drain fully after the cycle and avoid branches where liquid can sit stagnant.
Choose the skid pump using the whole circuit’s resistance, not just the size of the tank being cleaned.
Size Pumps From the Worst-Case Circuit, Not the Skid Tank Size
The supply pump must deliver the required cleaning flow after all losses through field piping, elevation, fittings, valves, heat exchangers, hoses, and the cleaning device.
A useful design relationship is:
Required pump duty point = validated cleaning flow at the object + total dynamic head of the complete supply circuit.
The return side should be checked separately for drainage, entrained air, foam, elevation, and vessel-bottom pooling.
Alfa Laval’s brewery CIP Q&A gives a practical example in which a tank requires 20,000 l/h while the line requires 32,000 l/h and notes that the objects are normally cleaned separately, with the higher line requirement controlling that cleaning duty. See Alfa Laval Brewery CIP Q&A.
Section 7: Mobile Fluid Dynamics for Boutique Production Floors
For small brewpubs, labs, or startups, a large fixed cleaning skid may not fit the space or the budget.
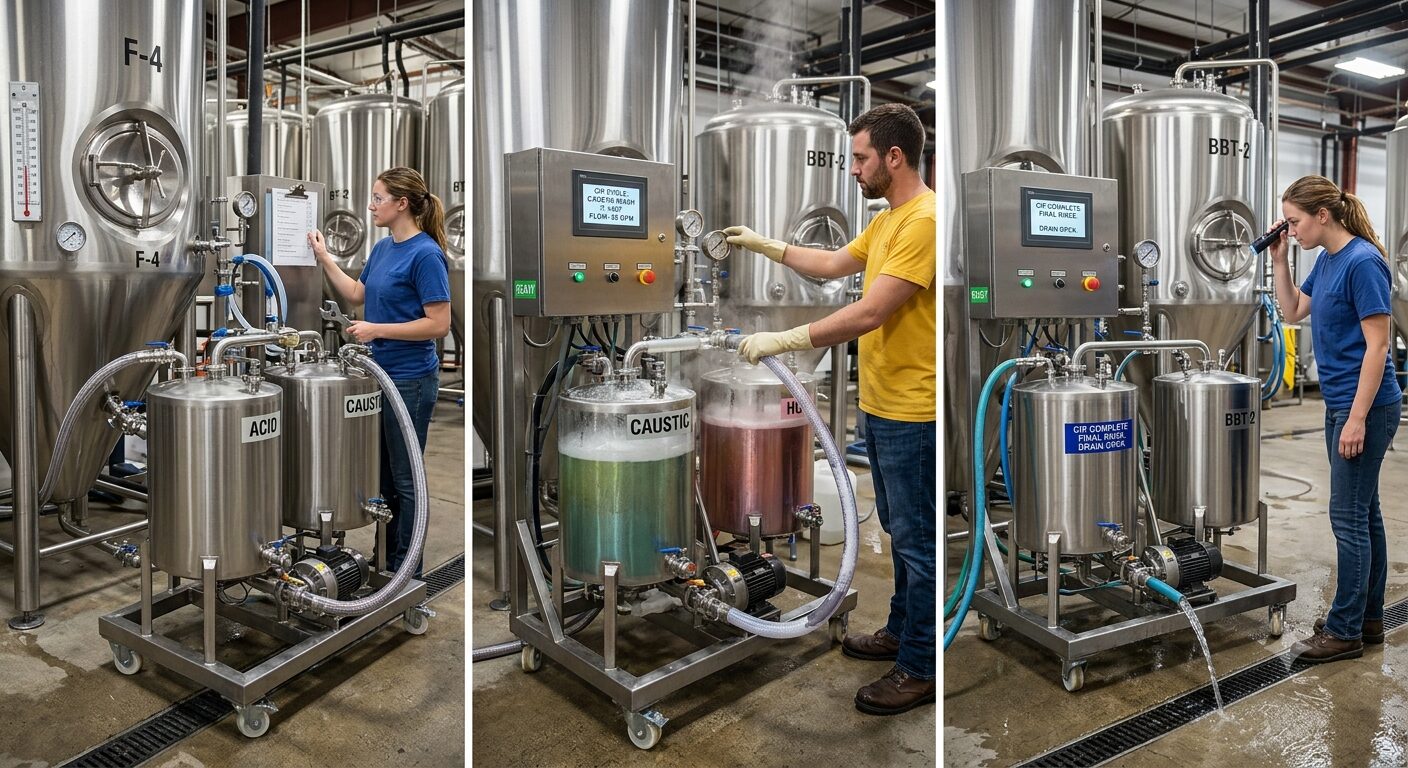
A flexible, mobile cip cart lets your crew roll cleaning power straight to any tank on the floor.
These carts have two compact steel tanks, a dedicated high-pressure supply pump, and built-in electric heating.
Your team can move the cart through tight tank rows and connect flexible hoses to close the cleaning loop.
This setup lets small companies automate tank washing without spending a fortune on fixed pipelines.
The built-in return pump keeps heavy chemicals flowing out of the tank base, so liquid does not pool during the wash.
With a heavy-duty mobile cart, small venues can reach industrial cleaning standards on a small budget.
Section 8: Chemical Thermodynamics and Active Formulation Selection
A truly clean inside surface needs the right brewery cip chemicals for each stage of the wash.
The main cleaning stage uses an alkaline compound, usually a strong caustic (sodium hydroxide) heated to about 140°F to 175°F.
This hot alkaline wash breaks down stubborn proteins, hop resins, and dead yeast stuck to the steel.
The second stage uses a phosphoric or nitric acid wash to dissolve minerals and beer stone.
The final stage uses a sanitizer, like peracetic acid, to kill any remaining microbes.
You must keep the chemical strengths and temperatures balanced to clean fully without damaging your lines.
To set safe wash temperatures and protect your staff, the Master Brewers Association of the Americas (MBAA) offers full cellar safety guides.
Managing Chemical Recovery on a Fixed Skid
Recovering chemicals saves money only when the returned solution is still effective.
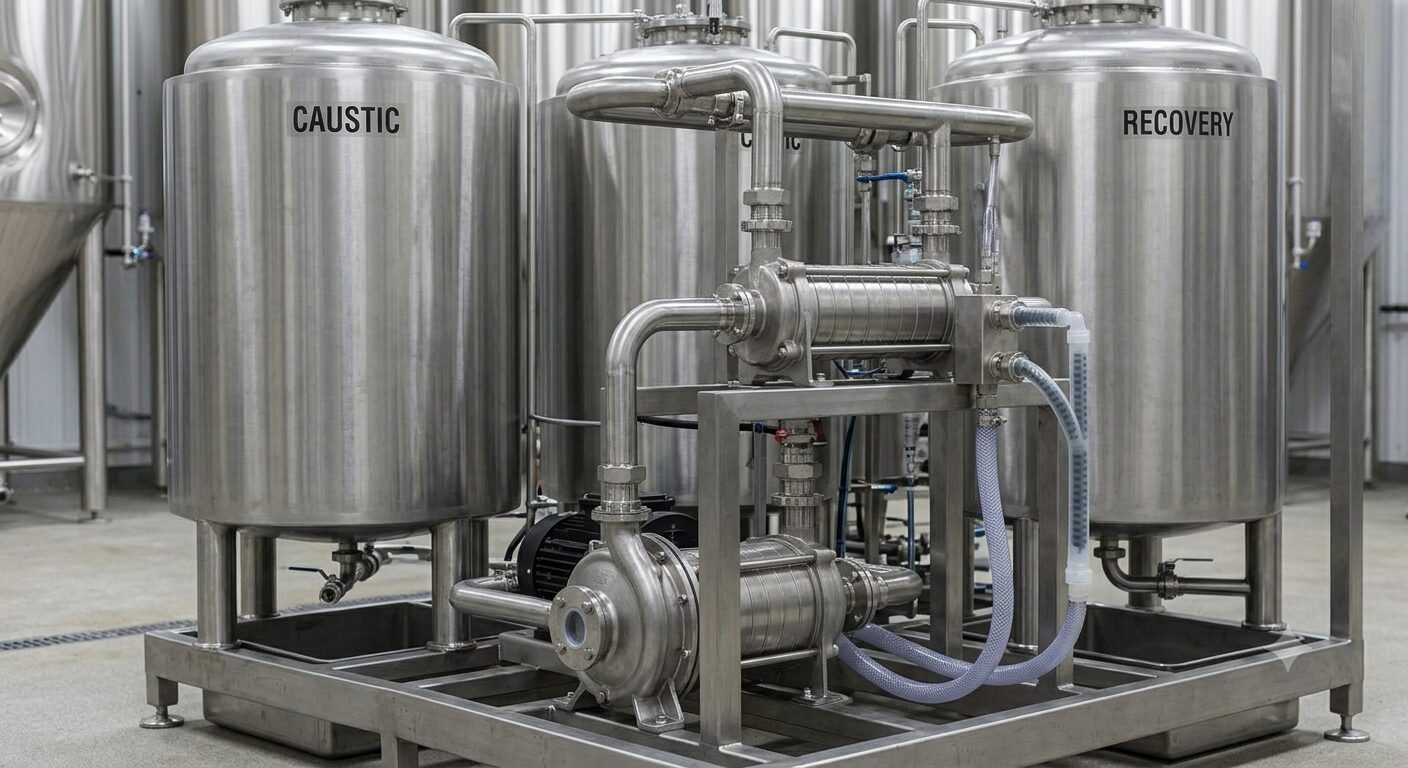
A fixed skid can return caustic and acid to their own storage tanks after circulation.
Before recovery, the system should check the destination and keep rinse water out of the wrong tank.
Conductivity, temperature, concentration checks, and a visual look help decide if a recovered solution is still good to reuse.
Every cycle adds water and removed soil, slowly changing the solution’s condition.
Set clear limits for dilution and contamination, and replace the solution once it falls outside them instead of correcting it forever.
Recovered Chemical Needs Defined Acceptance Criteria
Conductivity and a visual check are useful inputs, but they should not be the only basis for deciding whether every recovered cleaning solution remains suitable for reuse.
| Recovery Check | What to Define |
|---|---|
| Concentration | Conductivity correlation, titration, or another supplier-approved method. |
| Temperature | Acceptable storage and reuse range for the exact cleaning chemistry. |
| Soil loading | When dissolved or suspended contamination makes the solution unsuitable for another cycle. |
| Cross-contamination | Which brewery areas may share recovered solution and which must remain isolated. |
| Storage time | Maximum hold period and whether the solution needs retesting before reuse. |
| Dump logic | Automatic or operator criteria that route out-of-spec solution to the correct waste stream. |
Section 9: Quality Assurance and Microbiological Verification Protocols
To confirm your cleaning loops work, you need a strict cip cleaning validation routine.
You cannot just trust a visual check to confirm that a sealed steel pipe network is clean inside.
Modern validation programs use ATP bioluminescence swabs to detect trace organic material fast.
Teams collect samples from the final rinse and read them with a calibrated luminometer.
If the test shows a high light score, the system flags the loop as failed and forces a full re-wash.
Regular validation checks keep your cleaning routines hitting the strict standards needed for wholesale.
ATP Is a Verification Tool, Not Proof of Sterility
ATP gives a rapid indication of residual biological or organic material at the sampled point. A low ATP result does not by itself prove that the whole skid, field piping, or cleaned equipment is sterile.
EHEDG Guideline 50 covers hygienic design, management, and validation of CIP installations, and its automation guidance highlights the role of sensors in optimizing cleaning and preventing hygiene failures. See EHEDG Guideline 50.
A strong verification program can combine process records, conductivity or pH, visual inspection, ATP, targeted residue testing, microbiological checks, and periodic coverage testing as appropriate to the brewery’s risk.
To keep your layout safe and correctly piped, designs should follow the frameworks managed by the Deutscher Brauer-Bund.
Section 10: Standard Operating Procedures and Plant Floor Calendars
Building a top brand means organizing your daily floor work into a clear list of brewery cleaning procedures.
This master plan sets the exact chemical strengths, water volumes, and loop times for every vessel.
Bright tanks, wort chillers, yeast brinks, and fermenters all need wash profiles matched to their soil loads.
For example, a kettle needs a long, hot caustic wash for caramelized sugars, while a bright tank needs a low-temperature cycle to keep its gas pressure.
Your crew must log every wash cycle, noting temperature, chemical strength, and final validation scores in a database.
These strict records help directors find bottlenecks and trace any quality issue quickly.
For advice on gas safety and line-balance math, engineers use data compiled by the National Restaurant Association.
Section 11: System Infrastructure Performance Matrix
Choosing your core cleaning equipment means balancing upfront cost against daily labor hours.
The reference below shows what each equipment tier can do.
                           ┌──► Tanks: 2 x 50 gallon
[Mobile Two-Tank CIP Cart] ├──► Heating: internal electric immersion
                           └──► Best for: nano breweries and taprooms under 1,500 BBL/year
                                 ┌──► Tanks: 3 x 200 gallon
[Modular Multi-Tank Skid Layout] ├──► Heating: dedicated shell-and-tube steam exchanger
                                 └──► Best for: microbreweries and regional hubs up to 20,000 BBL/year
                                 ┌──► Tanks: 4+ x 1000 gallon
[Fully Automated Fixed Assembly] ├──► Heating: multi-zone steam loop with direct injection
                                 └──► Best for: industrial plants over 50,000 BBL/year
Determining the Correct Number of CIP Tanks
More CIP tanks do not automatically make a better system.
Choose the number of tanks after looking at your full cleaning schedule.
Work out water use, chemical recovery, heating needs, cycle time, and how many circuits you clean each day.
A larger multi-tank skid can heat or prepare the next solution while another phase is running.
But adding tanks also raises the footprint, cost, piping complexity, and maintenance.
The best skid supports your real production schedule without adding equipment you do not need.
Current Commercial Brewery CIP Skid Example
GEA currently offers its CIP-STAR Craft Station for small to medium breweries with 10 hl or 15 hl buffer-tank options, three detergent dosing pumps, and separate hot and cold feed lines that can support simultaneous brewhouse and cellar cleaning.
This is a supplier-specific configuration, not a universal rule for tank count. It is useful because it shows that a real skid is configured around cleaning duties and parallel operations rather than a simple barrels-per-year threshold. See GEA CIP-STAR Craft Station.
How to Choose the Number of CIP Tanks
| Process Need | Possible Effect on Tank Count |
|---|---|
| Single-use cleaning | Can reduce recovery storage but increases fresh water and chemical demand. |
| Recovered caustic | Normally needs dedicated storage plus routing and acceptance logic. |
| Separate acid recovery | Adds another dedicated vessel and contamination controls. |
| Rinse-water recovery | May justify a recovery or reclaimed-water tank. |
| Parallel cleaning circuits | Can require more working inventory or buffer capacity so one circuit does not starve another. |
| Hot and cold cleaning duties | May change tank, feed-line, or heat-exchanger configuration. |
Section 12: Metallurgical Standards and Bio-Security Washing Cycles
The metal blend and inside finish of your tanks affect how long beer stays fresh and how much cleaning costs.
Commercial tanks should be made from strong stainless steel, usually AISI 304 or acid-resistant AISI 316L.
These steels have plenty of chromium and nickel, which form a self-healing protective layer on the surface.
This layer guards the tank against cleaning acids, hard water, and the natural acids in fruit and hops.
To stop bacteria, the inside steel must be polished very smooth, with a roughness of 0.8 micrometers or less.
Rough spots, welds, or scratches can hide wild yeast and shield it from a normal loop cycle.
To study line sanitation models and cleaning validation, teams check the archives of the Institute of Brewing & Distilling (IBD).
Materials for Wetted and Non-Wetted Parts
Using the same steel grade for every part can raise the price without helping everywhere.
The material spec should separate wetted parts from the outer skid frame.
Tanks, sanitary pipes, valve bodies, pump chambers, and fittings that touch cleaning solution can be AISI 316 or 316L stainless steel.
These grades resist acids, chlorides, and repeated hot chemical cycles better.
The outer frame and non-contact parts can use AISI 304 when the environment allows.
Gaskets and seals must also match the chosen chemicals and temperatures.
Do Not Specify 316L for Every Wetted Part by Default
The 316/316L recommendation above can be appropriate for some chemical duties, but material selection should follow the actual chemistry, chloride level, temperature, concentration, welding, surface finish, and service life required.
Alfa Laval’s current CIP station literature describes sanitary design and modular construction without treating one universal stainless grade as the only acceptable answer for every brewery. The buyer should therefore request a material schedule that identifies the grade and elastomer for each wetted component and explains any areas where 316L is required instead of 304.

Section 13: Facility Safety and Environmental Compliance Frameworks
Running an industrial cleaning system means balancing heavy chemical use with strict local laws.
The high-pH caustic washes and low-pH acid rinses cannot flow straight into the city sewer.
To meet water safety laws, modern plants must fit a dedicated wastewater neutralization system.
This system collects your spent cleaning loops in a holding tank and uses probes to balance the pH before discharge.
Your crew must also wear full protective gear, including chemical-resistant suits, heavy gloves, and face shields.
By making safety and the environment a priority, you protect your staff and keep the plant running without legal delays.
CIP Skid Wastewater Requirements Are Site-Specific
The statement above that high-pH caustic and low-pH acid cannot flow straight into the city sewer is a useful conservative planning assumption, but the actual discharge requirements depend on the local sewer authority, pretreatment permit, wastewater flow, pH, organic loading, and applicable rules.
The skid design should therefore define recovery, drain segregation, equalization, neutralization, side-stream handling, and sampling points before the wastewater system is finalized.
What to Compare in a Brewery CIP Skid Quote
A professional quote should define the complete cleaning duty and installation scope rather than only skid tank count and pump horsepower.
| Quote Item | What to Confirm |
|---|---|
| Cleaning scope | All tanks, pipes, heat exchangers, fillers, brewhouse vessels, packaging circuits, and simultaneous cleaning requirements. |
| CIP tanks | Number, working volumes, water/caustic/acid/recovery duties, insulation, heating, drainage, and future expansion. |
| Pumps | Supply and return duty points, curves, VFDs, hygienic design, air handling, spare strategy, and worst-case circuit. |
| Heating | Steam/electrical load, heat exchanger, heat-up time, condensate, temperature control, and heat recovery. |
| Valve matrix | Route list, valve type, feedback, interlocks, mixproof requirements, maintenance mode, and isolation philosophy. |
| Instrumentation | Temperature, flow, pressure, conductivity, level, dosing, calibration, sample points, and alarm limits. |
| Automation | PLC/HMI, recipe permissions, data logging, alarm history, backups, remote support, and plant-control integration. |
| Recovery | Product, rinse-water, caustic and acid recovery; acceptance limits; phase separation; contamination control; and dump logic. |
| FAT / SAT / validation | Factory tests, site tests, worst-case circuits, cleaning acceptance criteria, documentation, and operator training. |
| Installation | Freight, rigging, anchoring, field piping, electrical work, utilities, commissioning, warranty, spare parts, and service. |
Brewery CIP Skid FAQ
What is a brewery CIP skid?
It is a fixed or modular clean-in-place station that stores, heats, pumps, doses, routes, recovers, and monitors cleaning solutions for brewery equipment and piping.
How many tanks should a brewery CIP skid have?
There is no universal number. Tank count depends on single-use versus recovery design, chemistry, simultaneous circuits, rinse-water reuse, hot/cold duties, and the brewery’s cleaning schedule.
How is a CIP skid pump sized?
Size the supply pump from the required validated cleaning flow and total dynamic head of the complete worst-case circuit, including field piping and the cleaning device.
Can one CIP skid clean several brewery areas at once?
Yes, when tanks, pumps, heating, feed/return lines, valve routing, and automation are specifically sized for simultaneous demand.
What does a valve matrix do?
It routes cleaning solution between the skid and different process areas while interlocks and valve feedback help prevent incompatible routes from opening together.
What is the difference between FAT and SAT for a CIP skid?
FAT verifies fabrication, controls, and simulated function at the supplier. SAT verifies real utilities, field piping, hydraulics, integration, and cleaning performance after installation.
Can a brewery CIP skid recover caustic and acid?
Yes, when the system has dedicated recovery storage and defined concentration, contamination, temperature, storage-time, and dump criteria.
Does ATP prove the CIP skid cleaned equipment to sterility?
No. ATP is a rapid hygiene indicator at the sampled point and should be used within a broader validation and verification program.
When should a brewery replace a mobile cart with a fixed CIP skid?
A fixed skid becomes more attractive when cleaning frequency, permanent circuits, simultaneous demand, recovery, labor, hose setup, and traceability make the mobile workflow a recurring bottleneck.
What should be included in a CIP skid supplier quote?
Compare cleaning scope, tanks, pumps, heating, valve routing, instrumentation, automation, recovery, FAT/SAT, validation, installation, utilities, commissioning, warranty, support, and spare parts.
Section 14: Final Summary and Operational Capital Deployment Blueprint
Choosing your core setup needs a clear view of your sales goals, your space, and your budget.
If you run a taproom where beer moves fast on-site, a compact mobile cart is an affordable start.
But if you want to grow wholesale across many states, a fully automated fixed skid is a must.
Check your building’s floor weight limits, balance your chemical strengths, and enforce strict validation loops.
Pick the right setup for your volume, treat your cleaning line as a key partner, and your team can keep delivering great beer.
Contact Us

Author | Operations & Sourcing Lead
Luca is an operations and sourcing specialist with extensive experience in project management and industrial manufacturing. This blog serves as a technical resource for brewery owners, offering clear guidance on equipment design, quality control, and supplier evaluation. In parallel, Luca advises international buyers on sourcing and importing brewing equipment—helping them manage risk, avoid costly mistakes, and achieve consistent production quality.
