
Read Time: ⏱️ 10 minutes | By: Luca
Brewery wastewater treatment begins with a clear picture of what reaches the drain. Brewing, fermentation, tank cleaning, packaging and utility operations produce streams with different flow, pH, temperature, solids and organic loads. A treatment system must manage this variation while meeting the requirements of the receiving sewer, discharge permit or approved reuse application.
The correct solution is not determined by brewery size alone. Two plants producing the same beer volume can have very different wastewater because of product losses, cleaning practice, packaging format, water efficiency and production schedule. Representative sampling and a time-based flow balance are therefore more useful than a generic capacity rule.
This article explains the measurements, process stages and operating decisions used to design and manage brewery effluent. It also separates municipal-sewer pretreatment from direct environmental discharge, because the two routes can require very different levels of treatment.
Brewery Wastewater Treatment at a Glance
| Design Question | Why It Matters |
|---|---|
| Where will the effluent go? | Municipal sewer, direct discharge and reuse follow different regulatory and treatment frameworks. |
| What are the average and peak flows? | Flow determines equalization volume, pump duty, hydraulic loading and retention time. |
| How strong is the wastewater? | BOD, COD and suspended solids determine the organic and solids loads imposed on treatment. |
| How variable are pH and temperature? | CIP discharges and hot rinses can upset downstream biological processes or exceed local limits. |
| Which side streams create peaks? | Yeast, trub, beer loss and first rinses can carry much more load than routine wash water. |
| What must the final effluent achieve? | The actual permit or sewer agreement defines the performance target and monitoring obligations. |
A useful design basis combines production records, flow monitoring, laboratory data and the discharge requirements issued for the site. Equipment selection should follow that work, not precede it.
Where Brewery Wastewater Comes From
Brewhouse wastewater can include vessel rinses, floor washing, spent-grain handling losses and wort spills. Cellar streams include yeast and trub removal, fermenter and bright-tank cleaning, beer losses and sanitizer rinses. Packaging adds bottle or can rinsing, filler cleaning, broken containers, label material and rejected product.
Clean-in-place systems create alternating alkaline, acidic and sanitizing streams. These may have extreme pH and can contain a substantial organic load when the first rinse carries beer, yeast or soil. Utility operations add filter backwash, cooling-system blowdown, boiler blowdown and water-treatment reject. These streams should be characterized separately because their chemistry differs.
Stormwater and uncontaminated cooling water should not automatically be mixed with process wastewater. Keeping clean water out of the process drain reduces hydraulic load and treatment cost, provided the separation complies with local plumbing and environmental rules.
Drain mapping is one of the most productive early tasks. Mark every source, destination, valve, sump and connection, then observe a full production cycle. The map helps identify cross-connections, avoidable water use and concentrated streams that may be recovered or managed separately.
Measure Flow and Load Before Selecting Equipment
Daily water consumption does not equal daily wastewater flow. Water leaves the site in packaged beer, evaporation, spent grain, waste solids and other routes. Conversely, stored water or cleaning solutions can create a discharge peak that is not visible in the daily total. Install or temporarily use flow measurement at representative points and relate the readings to the production schedule.
Record average daily flow, maximum day, peak hourly flow and short high-rate events. Note whether two operations can discharge simultaneously. Equalization and pumps must handle the real time pattern, while biological treatment is sized from both hydraulic and mass loading.
Mass load is calculated from concentration and flow. A moderate concentration at high flow can impose more load than a very strong but small stream. Use consistent units and have the treatment designer check conversions. Concentration alone is not a safe sizing basis.
Sampling should cover representative brew, cellar, packaging and cleaning periods. A single convenient grab sample may miss a yeast dump or capture only an unusual CIP event. Time-proportional or flow-proportional composite sampling can provide a more realistic average, while targeted grab samples reveal the strength of specific side streams.
Core Brewery Wastewater Parameters
| Parameter | What It Shows | Design Relevance |
|---|---|---|
| Flow | Wastewater volume over time | Hydraulic capacity, tanks, pumps and discharge reporting |
| pH | Acidic or alkaline condition | Neutralization, material compatibility and biological stability |
| BOD | Biodegradable oxygen demand | Biological load and possible sewer surcharge |
| COD | Chemically oxidizable matter | Rapid load trending and treatment balance |
| TSS | Suspended material | Screening, clarification, sludge production and discharge limits |
| Temperature | Thermal condition | Biological activity, safety and receiving-system limits |
| Nitrogen and phosphorus | Nutrient content | Biological balance or regulated nutrient removal |
| Conductivity | General dissolved-ion trend | CIP identification, salinity changes and reuse evaluation |
Laboratory methods and reporting limits should suit the permit and design purpose. BOD and COD are related but not interchangeable. Their ratio can help a designer understand biodegradability, yet it does not replace treatability testing when the wastewater contains unusual chemicals.
Additional tests may include fats, oil and grease, settleable solids, alkalinity, volatile fatty acids, sulfide, metals, specific cleaning chemicals or microbiological indicators. The receiving authority and process designer should determine which are relevant.
BOD, COD and Product Loss
Beer, wort, sugar and yeast are readily biodegradable, which is why small product losses can create a large wastewater load. BOD describes the oxygen used by microorganisms under the specified test conditions. COD uses a chemical method and is often available more quickly, making it useful for operational trending once its relationship with site-specific wastewater is understood.
The least expensive load is often the load that never enters the drain. Improve transfer recovery, maintain valves and seals, control filler rejects and collect concentrated product before rinsing. Dry cleanup of grain and solids also prevents material from becoming a pump, aeration and sludge-handling problem.
Track loss by process area and product volume. A rising COD load may reveal a leaking valve, inefficient transfer or packaging problem before the loss becomes obvious in finished-goods records. Wastewater data can therefore support both environmental performance and yield improvement.
Do not send concentrated alcohol, yeast or product to treatment without checking the design basis. A biological plant that handles normal wash water may be upset by an unexpected batch discharge. Establish a documented approval route for off-spec beer and large product losses.
Segregate High-Strength Side Streams
Yeast, trub, spent hops and the first product-rich rinse frequently represent a disproportionate share of the organic and suspended-solids load. Capturing these materials separately can reduce equalization volume, aeration demand, sludge generation and sewer charges.
The appropriate destination depends on composition, local rules and available outlets. Some material may be suitable for animal feed, digestion or another recovery route; other material requires controlled disposal. Never assume that a by-product is acceptable because it is food-derived.
Use clearly identified tanks, connections and procedures. Estimate storage from the largest credible event and collection schedule. Include secondary containment, ventilation, cleaning access and safeguards against accidental return to production.
Measure the result of segregation. Compare flow and mass load before and after the change, rather than relying only on reduced visual solids. Dissolved sugars and alcohol may remain even when the effluent looks clear.
Preliminary Treatment and Solids Capture
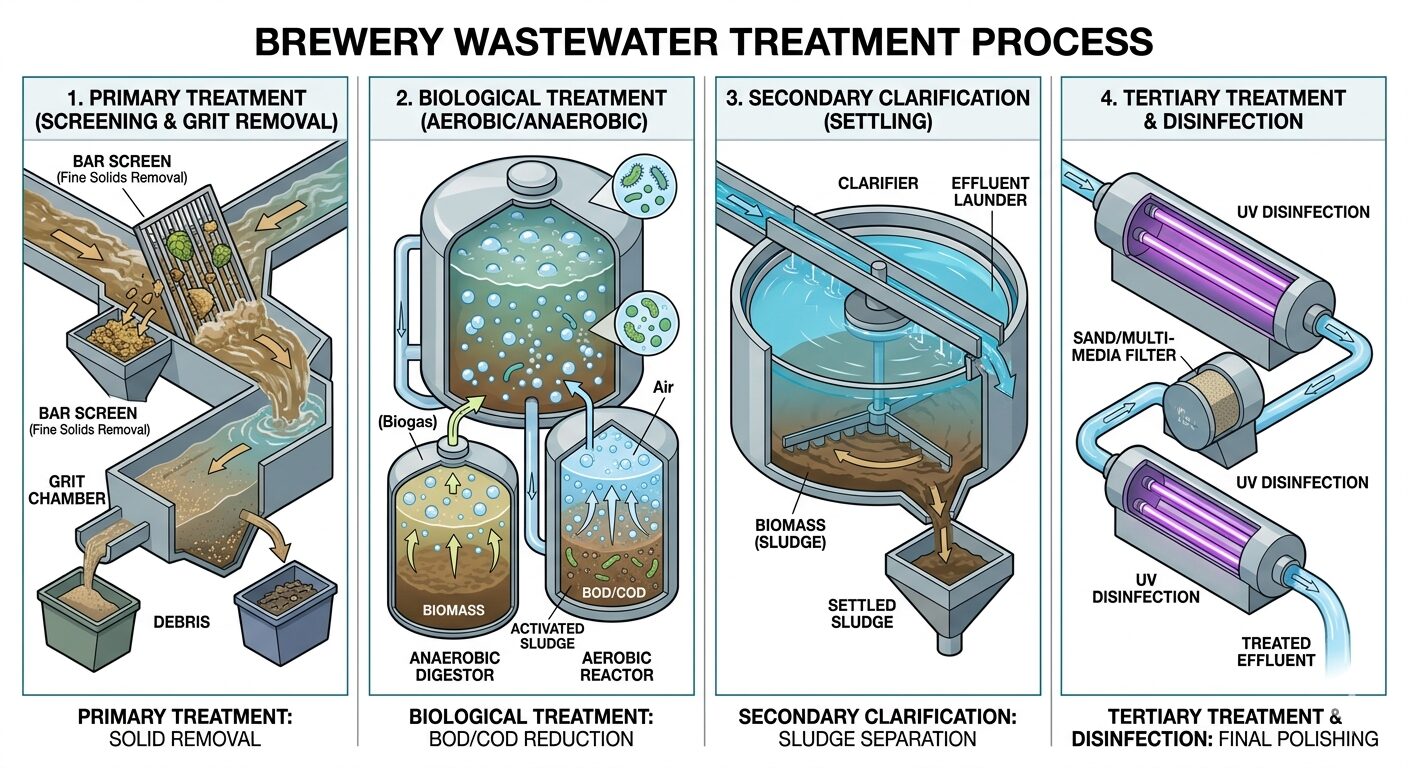
Screens, baskets or rotary strainers remove grain, hops, labels, glass fragments and other coarse material before it damages pumps or occupies tank volume. The opening size and equipment type should match the solids and flow. A screen that is too fine can blind rapidly; one that is too coarse passes material to the next stage.
Locate screening where operators can inspect and clean it safely. Provide drainage, lifting access and a hygienic way to contain screenings. Track the mass or volume removed because an increase can signal a process loss upstream.
Grit removal may be appropriate where soil, glass or dense particles occur. Grease separation is site-specific; brewery wastewater is not automatically high in fats and oils, but kitchens or food operations connected to the same system can change the requirement.
Screening does not remove dissolved BOD and is not a complete treatment system. Its value is protecting downstream equipment and keeping recoverable solids out of the liquid process.
Equalization for Variable Brewery Effluent
An equalization tank blends changing flow, concentration, pH and temperature. It protects downstream treatment from the sharp peaks created by CIP, packaging and product losses. Effective equalization is based on a time-series mass balance, not only a percentage of daily flow.
Mixing prevents settling and stratification. Aeration may be used for mixing and odor control, but it should be designed for the actual tank and wastewater. Excessive aeration wastes energy, while inadequate mixing allows solids to accumulate and anaerobic zones to form.
The tank needs usable working volume above settled solids and below overflow. Include high- and low-level protection, controlled discharge, emergency containment and access for inspection and cleaning. A bypass around equalization can defeat the entire treatment process and should be tightly controlled.
Long storage can lead to fermentation, acidification, sulfide formation and odor. Hydraulic retention must balance peak smoothing with wastewater stability. Monitor level, pH, temperature and, where useful, oxidation-reduction conditions.
pH Neutralization and CIP Management
Caustic cleaning solutions, acids and sanitizers can move brewery wastewater outside an acceptable pH range. Neutralization may be required before sewer discharge or biological treatment. The target range comes from the permit and the needs of downstream processes.
Automatic dosing requires reliable mixing, correctly located probes, chemical-compatible pumps and enough reaction time. A probe placed beside the chemical injection point can read a local concentration rather than the tank condition. Redundant measurement or an independent final check may be appropriate for a critical discharge.
Acid and caustic should not be combined casually. Neutralization releases heat and can create splashing or hazardous reactions with other chemicals. The system design must consider chemical compatibility, secondary containment, ventilation, eyewash, transfer connections and operator training.
Reusing a compatible spent acid or caustic stream for neutralization can reduce fresh chemical demand, but composition and control must be validated. Sanitizers and oxidants may affect biological treatment even after pH is corrected, so pH alone is not proof that a stream is safe to release.
Primary Solids Separation
Settling tanks, dissolved air flotation and other separation processes can reduce suspended solids before biological treatment. Their effectiveness depends on particle properties. Fine yeast, colloidal material and dissolved organics do not behave like heavy grain particles.
Dissolved air flotation introduces fine bubbles that attach to solids and float them for removal. Coagulants or polymers may improve separation when selected through testing. Chemical dose should be optimized rather than assumed, because overdosing increases cost and sludge and may harm downstream biology.
Clarifiers require suitable hydraulic loading, solids removal and sludge return or wasting controls. A compact separator with poor flow distribution may underperform despite adequate nominal area.
Primary treatment transfers pollutants from water into a sludge stream. Storage, dewatering, hauling and disposal must be included in the design and operating budget.
Aerobic Biological Treatment
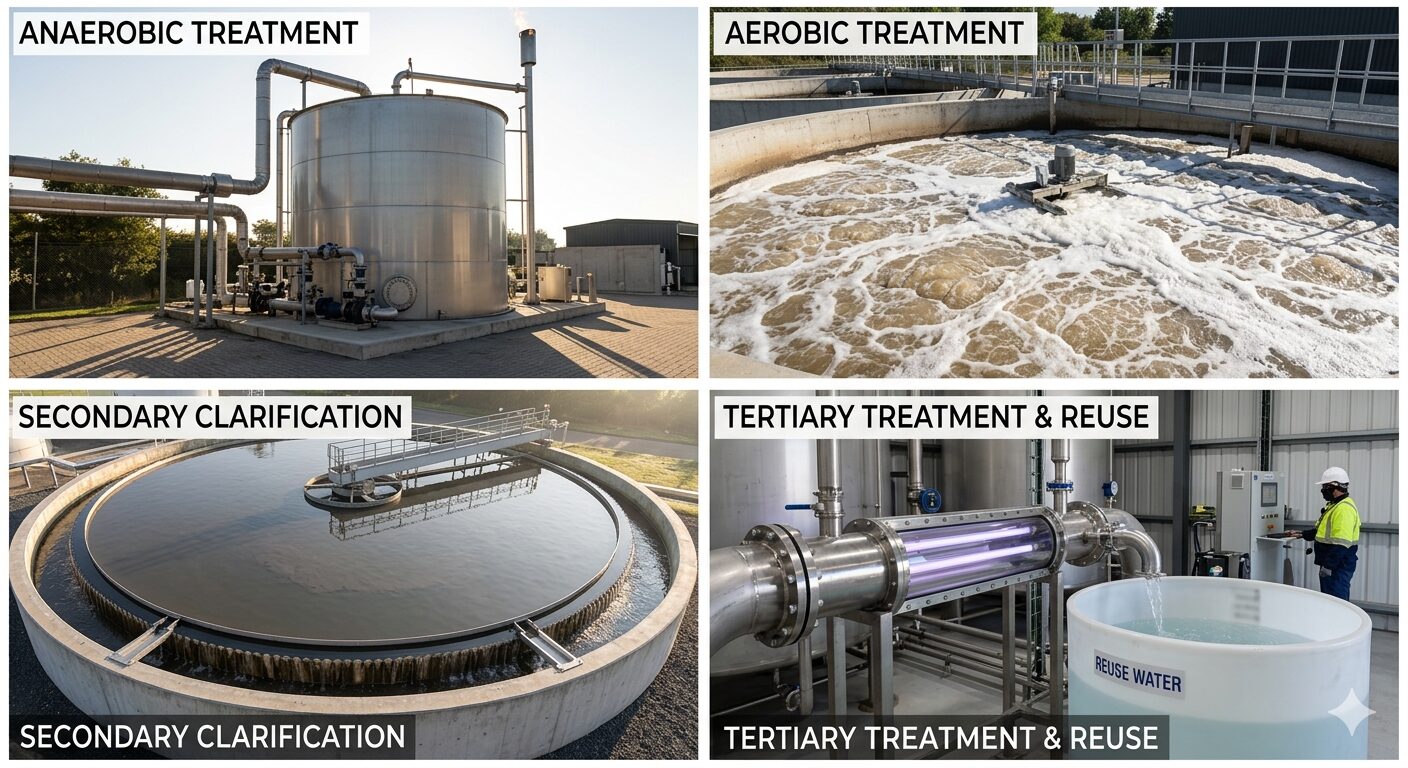
Aerobic processes use microorganisms and oxygen to reduce biodegradable organic matter. Activated sludge, sequencing batch reactors and moving bed biofilm reactors are among the options used for industrial wastewater. The choice depends on load, variability, footprint, effluent target and operator capability.
Aeration is often a major energy user. Oxygen transfer changes with tank depth, diffuser condition, temperature, salinity and wastewater characteristics. Size blowers and controls from actual oxygen demand and operating range rather than a generic power allowance.
Biological treatment needs a balanced environment. Excessive or deficient nutrients, extreme pH, toxic cleaning chemicals, rapid temperature change and shock loads can reduce performance. Brewery wastewater can be carbon-rich but nutrient balance still has to be assessed from measurements.
Monitor dissolved oxygen, pH, temperature, solids and the relevant process indicators. Microscopic or settling observations may assist activated-sludge operation. Effluent BOD or COD alone provides a delayed result; daily operational indicators help detect a problem earlier.
MBBR and SBR Options
A moving bed biofilm reactor uses suspended carrier media that provide surface for attached microorganisms. Retention screens keep the carriers in the reactor. The process can offer a compact biomass inventory and tolerate some load variation, but it still requires adequate pretreatment, mixing, aeration and solids separation.
Carrier fill fraction, protected surface area, oxygen delivery and hydraulic behavior are design variables. More media does not automatically create more usable capacity. Screens must remain clear and accessible, and the downstream process must remove biological solids released from the biofilm.
A sequencing batch reactor performs fill, react, settle and decant steps in a controlled cycle. It can combine biological treatment and clarification in one basin, but cycle timing, peak flow storage and reliable decanting are essential. Production schedules may influence the number and size of basins.
Neither acronym guarantees an effluent result. Ask suppliers for the design load, temperature range, oxygen requirement, sludge production, turndown, redundancy and performance guarantee.
Anaerobic Treatment and Biogas
Anaerobic microorganisms convert biodegradable organic matter without supplied oxygen, producing a gas containing methane and carbon dioxide. The technology can reduce aeration energy and recover energy where wastewater strength, flow and operating conditions justify the added complexity.
Anaerobic treatment is not automatically the best option for every brewery. Low or intermittent loading, cold wastewater, limited operating skill or inadequate gas use can weaken the business case. Treatability testing and a realistic mass-and-energy balance are important.
Stable loading, temperature, pH, alkalinity and nutrient conditions support the process. Rapid acidification or toxic chemical entry can upset the reactor. Equalization and controlled feeding are especially valuable.
Biogas systems require gas-tight equipment, pressure protection, condensate management, flame and explosion safety, gas monitoring and an approved use or flare. Methane emissions from leaks can undermine environmental benefits, so gas accounting must include collection efficiency.
Combining Anaerobic and Aerobic Treatment
For suitable high-strength wastewater, an anaerobic stage can remove a large part of the organic load before aerobic polishing. The aerobic stage then addresses remaining biodegradable matter and may support nitrification or other permit requirements.
The processes must be designed as one train. Anaerobic effluent characteristics affect downstream oxygen demand, nutrient balance, sulfide control and solids handling. Gas production and aerobic energy use should be calculated across the complete range of production.
Redundancy and bypass storage matter because the brewery cannot simply stop producing whenever one stage is unavailable. Define how high-strength streams will be held or diverted during maintenance without creating an uncontrolled discharge.
Membrane Bioreactors and Tertiary Polishing
A membrane bioreactor combines biological treatment with membrane solids separation. It can produce low-suspended-solids effluent in a compact footprint, but it requires membrane cleaning, air scour, screening and careful control of fouling.
Pressure, permeability, flux and cleaning frequency should be trended. A membrane barrier does not remove every dissolved contaminant and does not by itself make water suitable for unrestricted reuse.
Tertiary treatment may include media filtration, activated carbon, advanced membranes or disinfection. Select each barrier for a defined contaminant and final use. Adding equipment without a water-quality objective increases cost and maintenance without proving compliance.
Disinfection performance depends on the method, dose, contact conditions and water quality. Turbidity or suspended solids can shield microorganisms. Any residual disinfectant and by-products must also be compatible with discharge or reuse requirements.
Direct Discharge and Municipal Sewer Requirements
In the United States, direct point-source discharge to waters of the United States generally requires authorization under the National Pollutant Discharge Elimination System. Permit limits, monitoring and reporting are site-specific. The EPA NPDES permit information explains the general framework.
A brewery sending wastewater to a municipal sanitary sewer normally works with the local publicly owned treatment works or sewer authority. Local limits, pretreatment requirements, discharge permits, surcharges and reporting can apply. A sewer connection does not mean that any pH, temperature or organic load is acceptable.
Requirements outside the United States follow the national, regional and local authorities responsible for industrial discharge. Obtain the written limits for the exact site and receiving route. Do not design from a limit copied from another brewery.
Define sampling location, averaging period, analytical method, reporting frequency and response to noncompliance. A numerical limit without these details is not a complete compliance basis.
Nutrients, Sulfide and Odor Control
Nitrogen and phosphorus can be necessary for biological growth, deficient for a carbon-rich process or regulated in the final effluent. Laboratory analysis and process calculations determine whether nutrients need addition or removal. Uncontrolled nutrient dosing wastes chemicals and can increase discharge load.
Sulfide can form in stagnant, oxygen-poor wastewater containing sulfate. It causes odor, corrosion and serious safety concerns when hydrogen sulfide gas is released. Prevent long uncontrolled retention, maintain appropriate mixing and ventilation, and monitor where the risk assessment identifies a hazard.
Odor can also come from fermented product, volatile acids, sludge storage and uncovered screens. Good housekeeping, prompt solids removal and stable process operation usually come before complex odor-control equipment.
Enclosures and ventilation systems must not transfer an occupational hazard to another location. Gas detection, access control and confined-space procedures should follow the site risk assessment.
Sludge Handling and Residuals
Every solids-removal and biological process produces residuals. Estimate primary sludge, waste biological solids, screenings and chemical sludge across normal and peak operation. Include storage for collection interruptions and access for safe removal.
Thickening and dewatering reduce hauling volume but add equipment, polymers, wash water and labor. The best arrangement depends on disposal cost, site space and the receiving facility’s acceptance criteria.
Analyze residuals when required and keep manifests or records. Mixing incompatible residuals can make disposal more difficult. Prevent runoff and return drainage to an appropriate point in the treatment process.
Treated Water Reuse
Reuse begins by defining the use, not by selecting a filter. Floor washing, cooling makeup, toilet flushing, irrigation and process applications have different chemical, microbiological and regulatory requirements. Some uses may be prohibited or impractical at a particular site.
Use a risk-based multi-barrier approach. Biological treatment, solids separation, filtration and disinfection may all be needed, followed by storage and distribution designed to prevent recontamination.
Keep reuse water physically separated from potable and product systems. Apply identification, backflow prevention and controlled connection practices. An accidental cross-connection can outweigh the water savings.
Monitor the parameters relevant to the final use and define an automatic diversion when quality is outside specification. Reuse volume should be matched with demand; producing polished water without a reliable user creates storage and disposal problems.
Wastewater Reduction Inside the Brewery
Start with dry cleanup, repaired leaks, controlled hose nozzles and clear shutdown procedures. Improve vessel emptying before rinse and capture the first high-strength rinse where practical. Optimize CIP from validated cleanliness rather than shortening cycles without evidence.
Flow meters on major users help separate water efficiency from production changes. Report water use and wastewater load per consistent production unit, while also retaining absolute totals. A ratio can improve even when total impact rises with production.
Review packaging rejects, filler setup, tank transfers and beer recovery. Product sent to the drain is both lost revenue and treatment load. Connect environmental indicators with production yield.
The Brewers Association water and wastewater resource provides brewery-specific material on reduction and management practices.
Instrumentation and Process Control
Typical measurements include influent and effluent flow, tank level, pH, temperature, dissolved oxygen, conductivity, pressure and blower or pump status. Online instruments support control but must be calibrated, cleaned and checked against appropriate standards or laboratory results.
Alarm design should identify the action required. High tank level may stop an upstream transfer; low dissolved oxygen may increase aeration or trigger an investigation; out-of-range final pH may divert discharge to equalization.
Protect critical settings and record changes. Trend data with production events, chemical use and laboratory results. This makes it possible to distinguish an instrument fault from a genuine process change.

Sampling, Laboratory Testing and Records
Create a written sampling plan with locations, methods, containers, preservation, holding times and responsibilities. Samples must represent the regulated discharge and the purpose of the analysis. Follow the permit and laboratory instructions.
Use accredited or otherwise approved laboratories where required. Review quality-control flags and detection limits rather than copying only the reported number. A non-detect result above the permit limit is not useful evidence of compliance.
Maintain flow, production, chemical, sludge, maintenance, calibration and analytical records. Investigate trends before a limit is exceeded. Document corrective action and verify that it worked.
Safety in Brewery Wastewater Treatment
Wastewater facilities combine chemicals, electrical equipment, moving machinery, wet surfaces, pressure, biological aerosols and potentially hazardous gases. Complete a task-based risk assessment and develop procedures for normal operation, sampling, cleaning and maintenance.
Personal protective equipment depends on the chemical safety data and task. It does not replace closed transfer, guarding, ventilation, secondary containment, eyewash, emergency shower and lockout controls.
Tanks, pits and enclosed treatment spaces may meet the definition of a confined space. Entry requires the applicable permit, isolation, atmospheric testing, rescue planning and trained personnel.
Never mix chemicals unless the procedure and compatibility have been reviewed. Label tanks and transfer points and prevent a delivery from being connected to the wrong system.
Data Needed to Size a Brewery Wastewater System
- Flow profile: average, maximum day, peak hour and simultaneous discharges.
- Organic load: representative BOD and COD concentrations and mass per day.
- Solids: TSS, settleable material and the sources of screenings and sludge.
- pH and temperature: complete ranges during production and CIP.
- Nutrients and inhibitors: nitrogen, phosphorus, salinity, oxidants and relevant cleaning chemicals.
- Schedule: brew, packaging, cleaning, shutdown and seasonal patterns.
- Discharge target: permit, sewer agreement, surcharge thresholds or reuse specification.
- Site conditions: footprint, elevation, drainage, utilities, access, odor receptors and flood risk.
- Operating resources: staffing, laboratory support, maintenance capability and automation needs.
Provide raw data and sampling context to suppliers. Average values without peaks can produce an undersized system, while isolated worst-case samples without frequency can cause unnecessary oversizing.
Brewery Wastewater Treatment Options Compared
| Process | Main Function | Important Limitation |
|---|---|---|
| Screening | Captures coarse solids | Does not remove dissolved organic load |
| Equalization | Balances flow, pH and load | Requires mixing, volume and odor control |
| Neutralization | Controls acidic and alkaline discharge | Does not remove BOD simply by correcting pH |
| DAF or clarification | Separates suspended and floatable matter | Creates sludge and may require chemicals |
| Aerobic treatment | Reduces biodegradable organic load | Needs oxygen, process control and sludge handling |
| Anaerobic treatment | Reduces strong organic load and can produce biogas | Requires suitable scale, stable operation and gas safety |
| MBR | Provides biological treatment and membrane solids separation | Requires fouling control, cleaning and energy |
| Tertiary treatment | Polishes effluent for a defined target | Must be matched to the remaining contaminants |
What Drives Brewery Wastewater Treatment Cost?
Capital cost depends on flow, load, treatment target, civil work, building needs, redundancy, automation, odor control and sludge facilities. Operating cost includes electricity, chemicals, laboratory testing, labor, maintenance, replacement parts and residual disposal.
Compare proposals on the same design basis. One supplier may exclude equalization, installation or sludge handling while another includes them. Clarify battery limits, utilities, foundations, piping, electrical work, commissioning and performance testing.
Evaluate the cost of risk as well as equipment. Insufficient storage, no standby pump or limited service support can create production interruption or discharge noncompliance. Redundancy should reflect consequence and repair time.
Potential savings include lower sewer surcharges, reduced product loss, water reuse and energy recovery. Use measured loads, local tariffs and realistic uptime rather than universal payback claims.
Supplier Evaluation and Performance Guarantees
A useful quotation states influent design ranges, hydraulic and mass loads, effluent targets, operating temperature, required chemicals, power, sludge production and operator attention. It should explain what happens outside the design envelope.
Ask for process calculations, equipment data, materials, control philosophy, alarm list, layout, maintenance access and references from comparable wastewater. Confirm local service and critical spare-part availability.
Performance guarantees need a defined test period, sampling method, production conditions and responsibility for laboratory analysis. The brewery must operate within the agreed influent range during the test.
Used tanks or equipment may be suitable after inspection, but unknown coatings, corrosion, trapped residues and incompatible materials can create risk. Confirm structural, chemical and process suitability before purchase.
Commissioning and Acceptance Testing
Commissioning verifies installation, flow direction, valve position, pump rotation, instruments, alarms, interlocks, chemical systems, ventilation and emergency controls. Water testing should precede introduction of wastewater where practical.
Biological processes require startup and biomass development. Performance may not be immediate, and the plan should define temporary discharge arrangements and load ramping. Track the conditions that affect acclimation.
Acceptance testing should use representative production and the agreed analytical methods. Verify hydraulic capacity, equalization, pH control, treatment performance, sludge handling, data logging and final discharge diversion.
Handover includes drawings, operating procedures, calibration records, equipment manuals, control backups, spare parts, training and emergency contacts. Update documents after field changes.

Connect Wastewater Control With Brewery Operations
Wastewater performance improves when the treatment team can see the brewing and cleaning schedule. Planned yeast removal, packaging sanitation and clean-in-place operations can then be distributed to avoid several strong discharges arriving at equalization together.
Changes to recipes, production volume, cleaning chemicals or brewery water treatment can alter effluent flow, conductivity, pH or nutrient balance. Include wastewater review in the approval process for operational changes rather than waiting for a discharge result to reveal the effect.
Hold a regular review of water use, product loss, chemical consumption, laboratory results, sludge production, alarms and maintenance. Assign each unusual event to a production cause where possible and confirm that corrective action improved the next comparable cycle.
This shared operating view helps the brewery reduce load at the source while keeping treatment stable. It also provides better evidence for capacity planning when a new fermenter, packaging line or production shift is proposed.
Brewery Wastewater Treatment FAQ
What is brewery wastewater treatment?
It is the collection and processing of brewery effluent to control solids, organic load, pH, temperature, nutrients and other relevant pollutants before discharge or approved reuse.
Why does brewery wastewater have high BOD?
Wort, beer, sugar, alcohol and yeast are biodegradable. Product losses and concentrated first rinses can therefore create substantial oxygen demand.
Which wastewater parameters should a brewery test?
Common parameters include flow, pH, BOD, COD, TSS and temperature. Nitrogen, phosphorus, conductivity, sulfide or specific chemicals may also be relevant to the process or permit.
Does every brewery need a complete biological plant?
No. The required treatment depends on the discharge route, local limits, wastewater load and receiving facility. Some sewered breweries need source reduction and pretreatment, while direct discharge generally requires more complete treatment.
What is the purpose of equalization?
Equalization blends variations in flow, organic concentration, pH and temperature so downstream processes receive a more stable load.
What is the difference between aerobic and anaerobic treatment?
Aerobic processes supply oxygen to microorganisms. Anaerobic processes operate without supplied oxygen and can produce methane-rich biogas from suitable high-strength wastewater.
Can treated brewery wastewater be reused?
Potentially, when the intended use is permitted and the treatment, monitoring, storage and distribution system meet its chemical and microbiological requirements.
How is a brewery wastewater system sized?
It is sized from time-based flow, pollutant mass loads, variability, temperature, discharge targets, operating schedule and site constraints, supported by representative sampling.
How much does brewery wastewater treatment cost?
There is no universal price. Flow, organic load, solids, limits, civil work, automation, sludge management, energy, chemicals and labor all affect capital and lifetime cost.
What should a treatment supplier guarantee?
The proposal should define the influent design envelope, hydraulic capacity, effluent target, test method, operating conditions and exclusions, along with utilities and expected residual production.
Planning a Reliable Brewery Effluent System
Begin with the discharge authority, drain map, production schedule and representative laboratory data. Reduce avoidable product and solids losses before calculating treatment capacity.
Choose each process for a measured load and defined performance target. Include operator capability, maintenance, sludge handling, safety and response to abnormal production in the design.
A reliable system is not simply a reactor or skid. It is a controlled path from every brewery drain to a verified discharge point, supported by monitoring, records and procedures that remain effective as production changes.
Contact Us

Author | Operations & Sourcing Lead
Luca is an operations and sourcing specialist with extensive experience in project management and industrial manufacturing. This blog serves as a technical resource for brewery owners, offering clear guidance on equipment design, quality control, and supplier evaluation. In parallel, Luca advises international buyers on sourcing and importing brewing equipment—helping them manage risk, avoid costly mistakes, and achieve consistent production quality.
